 EN
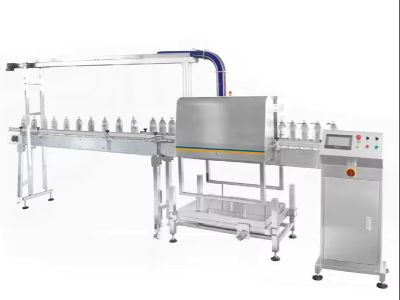
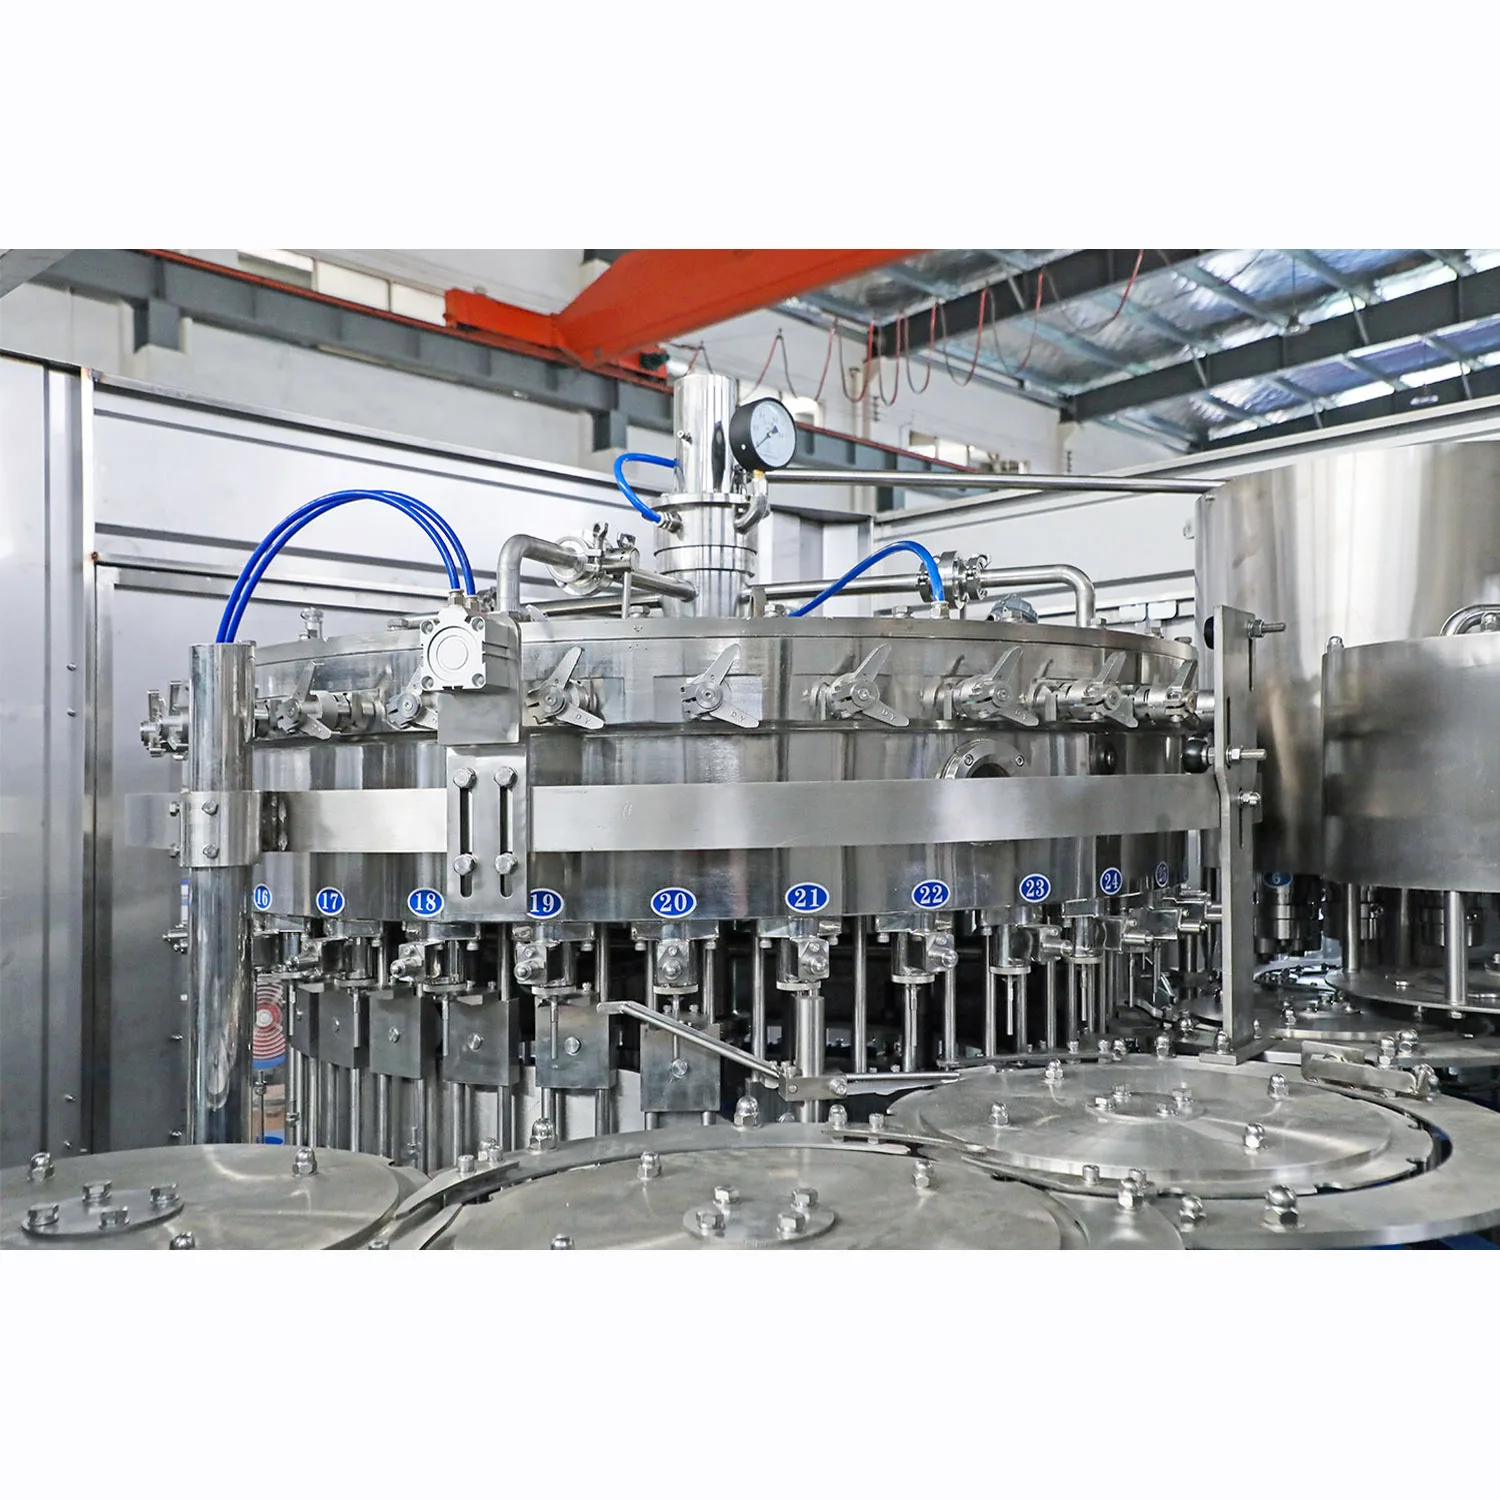
Monoblock filling machines are essential equipment for companies in the beverage, dairy, and food industries, offering an efficient solution for filling, capping, and labeling in a single unit. For B2B buyers, the selection of the right monoblock filling machine is crucial as it directly impacts production efficiency, product quality, and overall operational costs. This article will help you navigate the key considerations for choosing a monoblock filling machine, evaluate its quality, find reliable suppliers, and understand its applications across various industries.
How to Evaluate the Quality of Monoblock Filling Machines for Wholesale
To ensure you are investing in a quality monoblock filling machine, begin by examining the manufacturer's certifications. Look for ISO9001 and CE certifications, which indicate adherence to international quality management standards and safety regulations. These certifications can provide assurance that the machine has been tested for quality and reliability.
Next, review the machine's technical specifications. Key parameters include filling accuracy, speed, and the range of bottle sizes it can accommodate. High filling accuracy is essential to minimize product waste and ensure customer satisfaction.
Additionally, consider conducting a quality inspection of the machine. This process might involve reviewing material specifications, operational tests, and obtaining references from other clients. It's advisable to visit the manufacturer's facility if possible to see the production and quality control processes in action. A trial run with a sample before mass production can also highlight any potential issues early in the process.