 EN
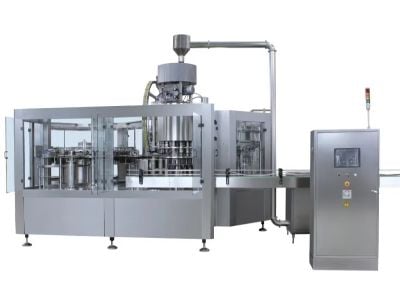
Monoblock liquid filling machines are essential for businesses in the beverage, dairy, and other liquid industries, streamlining the filling and packaging processes into a single, efficient system. For B2B buyers, understanding the advantages of these machines, their quality indicators, and sourcing options is crucial when making purchasing decisions. This article will explore key considerations for selecting a monoblock liquid filling machine, addressing common buyer concerns and providing practical insights to facilitate informed choices.
Evaluating the Quality of Monoblock Liquid Filling Machines for Bulk Orders
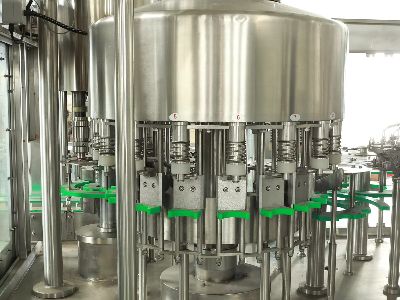
When considering bulk orders of monoblock liquid filling machines, quality evaluation is paramount. Key quality indicators include the materials used in construction, the machine's compliance with industry standards, and the reputation of the manufacturer. For instance, machines constructed from stainless steel offer durability and ease of cleaning, which is essential for maintaining hygiene in food and beverage production.
Buyers should also assess the manufacturer's certifications, such as ISO9001 and CE, which indicate adherence to international quality standards. Furthermore, inspecting previous projects or obtaining references can provide insights into the supplier's reliability and the performance of their machines in real-world applications.
Testing the machine's performance through samples or trials is another effective way to evaluate quality. This can include assessing the machine's filling accuracy, speed, and ease of operation—ensuring that it meets the specific requirements of your production line.