 EN
Bottle air conveyors are essential systems used in the beverage and liquid packaging industries to transport empty bottles through various stages of production. These systems help optimize workflow and ensure efficient handling of bottles while minimizing breakage and contamination risks. For purchasing managers and distributors, understanding the quality, installation, and maintenance of bottle air conveyors is crucial to ensuring smooth operations in production lines. This article aims to equip buyers with the necessary insights into evaluating and selecting bottle air conveyors that meet their specific needs.
Finding Trusted Bottle Air Conveyor Manufacturers
Finding a reputable bottle air conveyor manufacturer is crucial for ensuring quality and reliability in your production processes. Start by researching manufacturers with a proven track record in the beverage and liquid packaging sector. Look for companies that have been in operation for several years and have experience exporting to different markets.
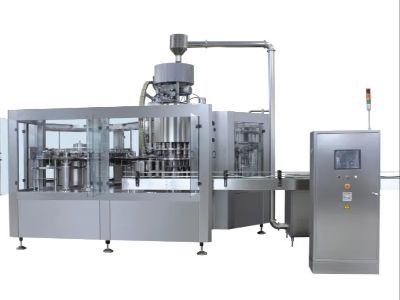
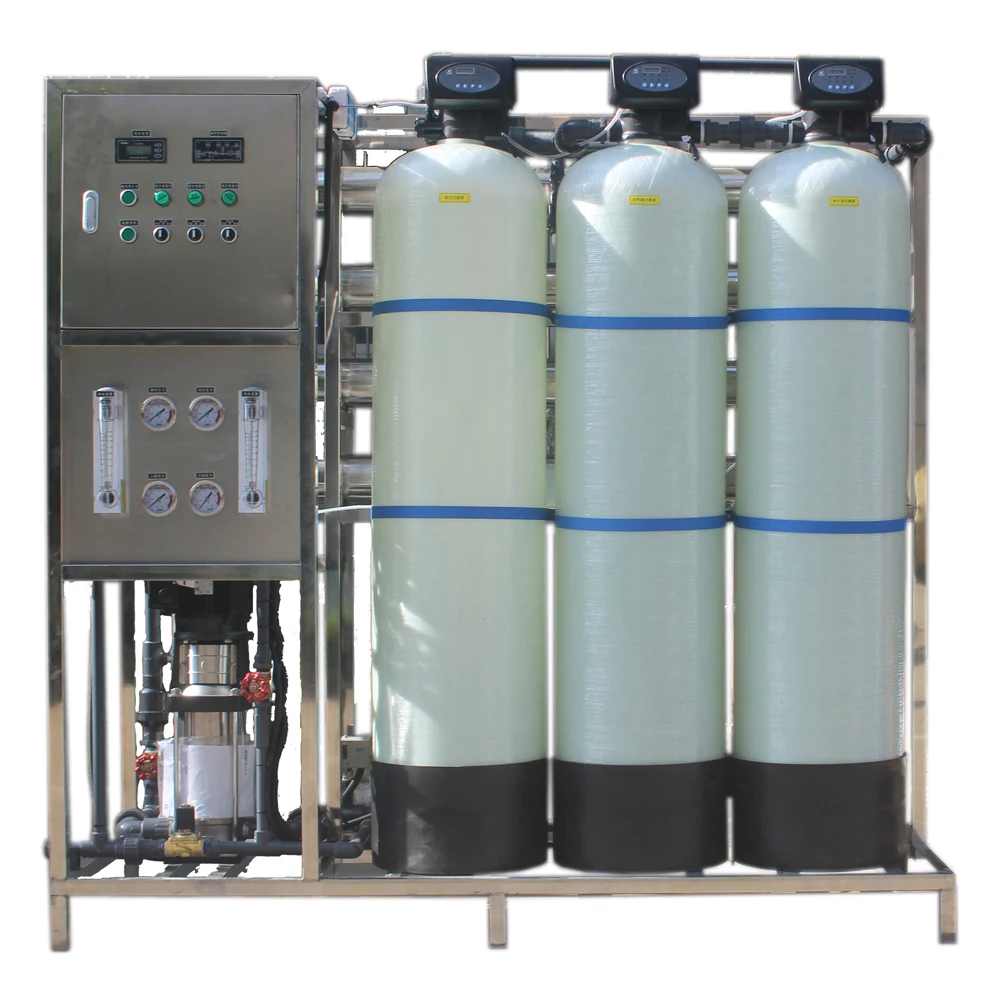
Check for industry certifications, such as ISO9001 and CE, which demonstrate a commitment to quality and safety standards. Additionally, seek manufacturers with in-house engineering teams capable of providing customized solutions tailored to your specific needs. This can be particularly beneficial if your production line has unique requirements or if you need assistance with installation and maintenance. For example, the A to Z Complete Full Automatic Mineral Water Plant Machine Project showcases a manufacturer’s ability to cater to specific requirements.
Networking within industry forums and trade shows can also help you connect with reputable manufacturers. Engaging with peers who have firsthand experience can provide valuable insights and recommendations. Finally, request quotes and compare pricing, lead times, and after-sales support to ensure you partner with a manufacturer that aligns with your operational goals.